

PHOENiX Sample · 3 min read · Last updated
A sample that looks wrong may have a surface defect rather than a shade error. Streaks, craters, pinholes or local texture changes can alter the visual impression and make instrumental readings less representative. Correcting the pigment balance before understanding the defect can create a second problem while leaving the first one unresolved.
A disciplined investigation begins with a description of what is visible, where it occurs and which process conditions are associated with it.
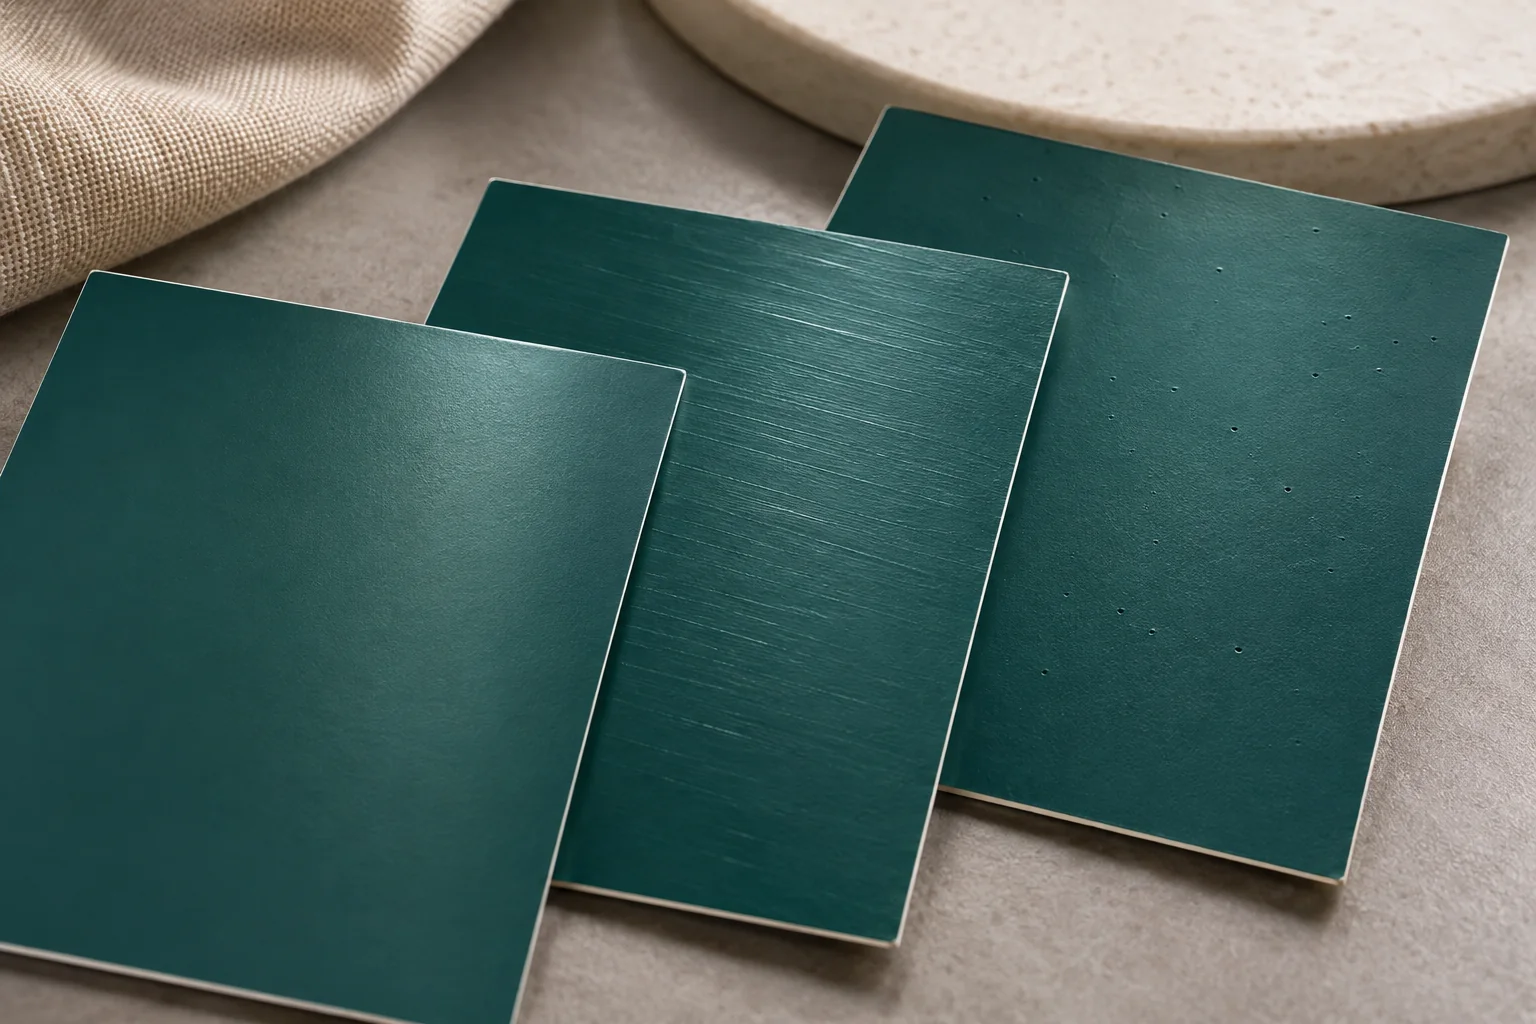
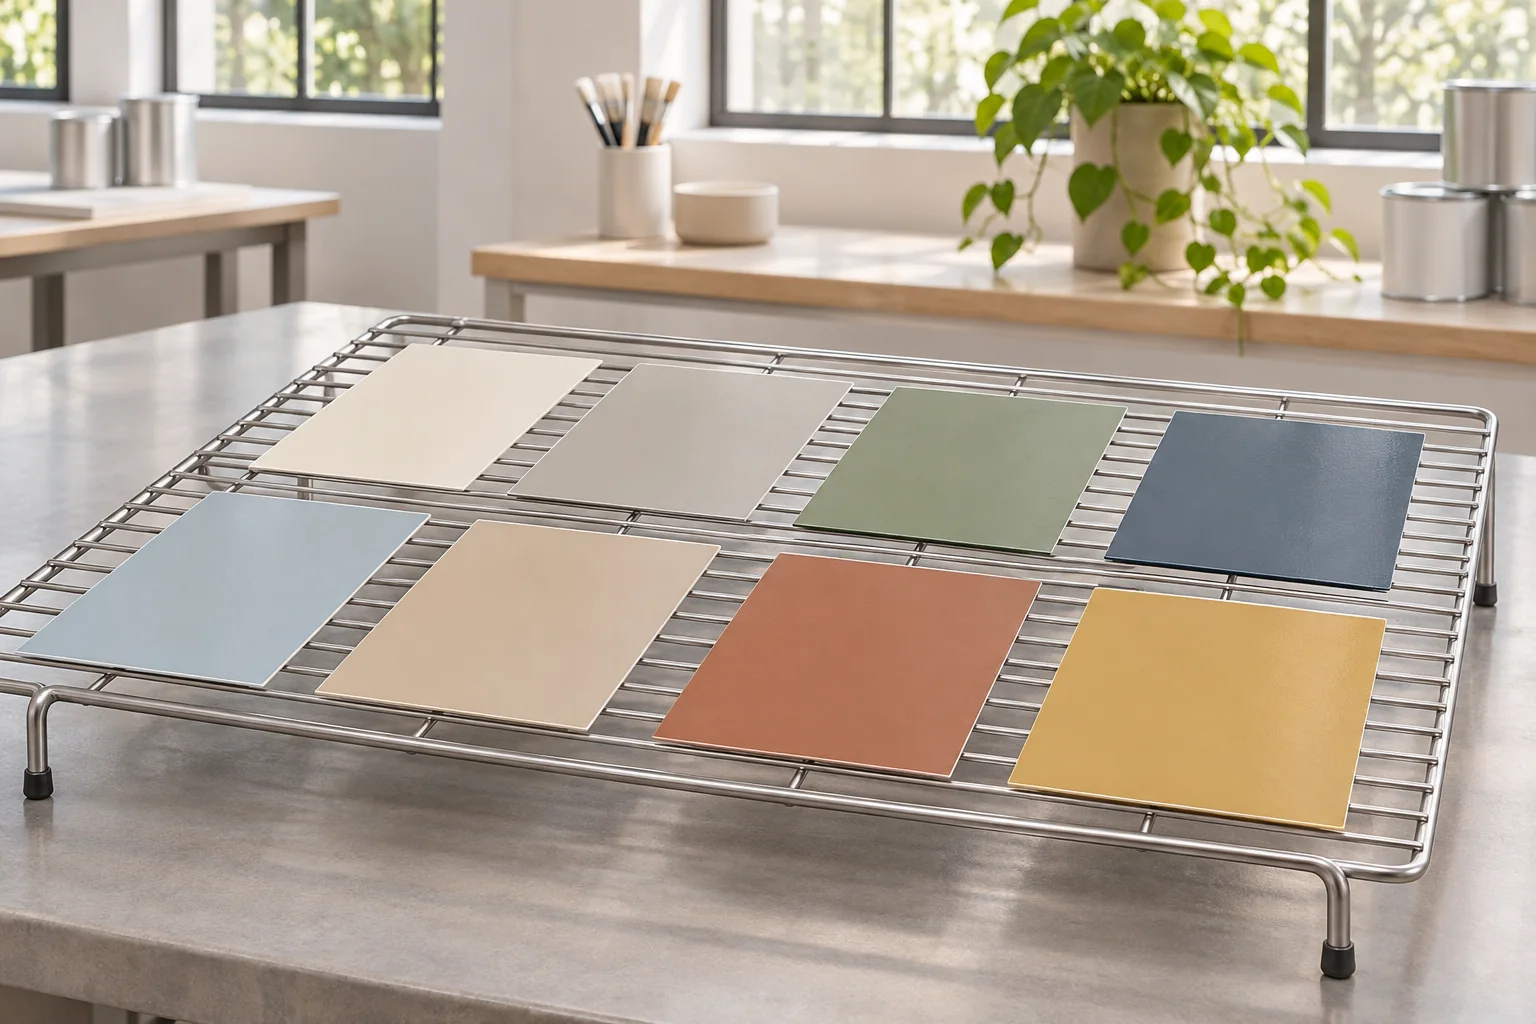
AI-generated concept illustration: Painted cards with differing surface uniformity.
Describe the symptom without assuming the cause
Use consistent terms and photographs to document the surface. Record whether the defect is local or widespread, repeated in a direction, concentrated near an edge or associated with a particular operation. Preserve representative samples where practical.
BYK's discussion of surface defects identifies several mechanisms and appearances, including cratering and leveling problems. BASF's technical description of craters highlights the role that small amounts of contamination can play. These references support investigation, but a similar-looking mark is not proof of a particular cause in every coating system. [1] [2]
Read the pattern across the process
Compare samples from before and after the point where the defect appears. Examine the substrate, preparation, application, drying and handling sequence. If the defect occurs only after conversion or stacking, the investigation should include those operations rather than remaining confined to the coating mix.
Keep changes controlled. Adjusting the substrate, application speed and formulation simultaneously may produce a better sample but leave the team unable to explain why. A repeatable correction requires evidence about the relevant variable.
Separate local defects from representative color
A measurement area containing a crater, scratch or uneven film may not represent the intended coating. Follow the agreed inspection and measurement procedure, and record why a region was excluded if exclusion is permitted. Do not select only the best-looking spot to conceal a nonuniform sheet.
If uniformity is part of the product requirement, inspect it as a separate attribute. An average color value can be acceptable while the sample remains visibly unsuitable for presentation. The quality decision should acknowledge both observations.
Use a structured investigation log
| Observation | Next comparison |
|---|---|
| Directional streaking | Application direction and equipment condition |
| Local depressions or craters | Surface preparation and contamination possibilities |
| Fine holes or bubbles | Relevant material and process history |
| Marks appearing after stacking | Conditioning and contact conditions |
These are routes for investigation, not automatic diagnoses. The coating supplier or qualified technical team should assess formulation changes and material compatibility. An editorial guide should not prescribe an additive or dosage from a photograph of a defect.
Verify the correction in the finished construction
After a controlled change, compare a new trial with the retained defect sample and the approved appearance reference. Repeat the relevant downstream operations to confirm that the issue does not return during cutting, assembly or packaging.
Test a suspected preparation change
Coat paired specimens from one substrate lot. Prepare one with the current method and the other with the proposed cleaning method. Keep coating, applicator and drying conditions fixed. Inspect equal areas under the same light and record crater counts and locations. Repeat with fresh specimens. If counts fall consistently, verify the change on an assembled sample. The result supports the preparation change, while identifying the contaminant requires separate evidence. BASF — Crater defects
Practical conclusion
Document the accepted process condition and the reason for the decision. The useful outcome is more than a cleaner-looking sample: it is a correction that can be reproduced and monitored. Treating surface defects as evidence about the process leads to better decisions than labeling every appearance problem a color mismatch.